


Pneumatically Actuated Ball Valves for Chemical Processing
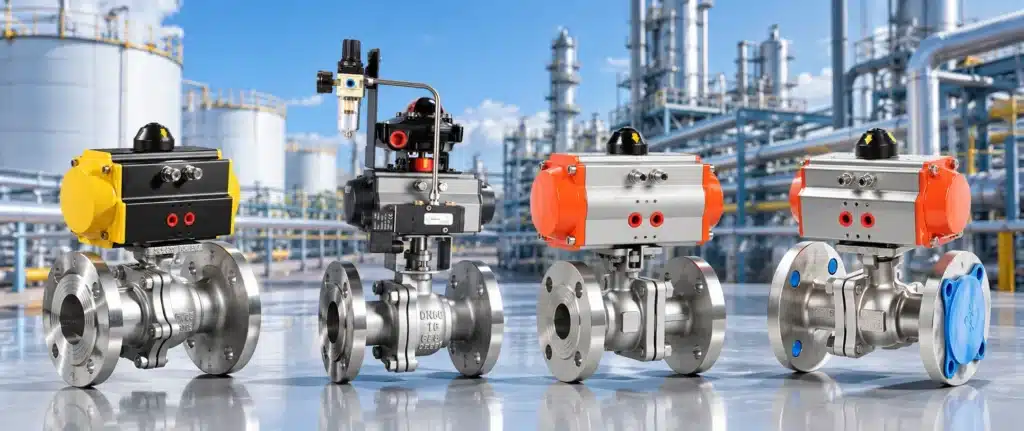
Pneumatically actuated ball valves are widely used in chemical processing systems for automated isolation, chemical transfer, dosing, tank switching and process sequencing. Their quarter-turn construction provides fast operation, while pneumatic actuators allow the valve to be controlled remotely without requiring an operator at the pipeline.
Chemical service, however, places more demanding requirements on a valve than general water or utility applications. Acids, alkalis, salts, solvents, oxidizing chemicals and concentrated process fluids can attack valve bodies, seats, seals and stems if materials are selected incorrectly.
For this reason, selecting pneumatically actuated ball valves for chemical processing requires more than matching the valve size to the pipeline. Engineers must consider chemical compatibility, concentration, temperature, pressure, solids content, actuator configuration, fail position and maintenance requirements as one complete system.
This guide explains how pneumatically actuated ball valves are used in chemical plants, which materials are commonly considered for corrosive service, where plastic and stainless-steel valves differ, how fail-safe pneumatic actuation works and what information should be provided when specifying a chemical-service valve.
There is no single valve material that is suitable for every chemical. Always evaluate the exact chemical name, concentration, temperature, pressure and contamination level before selecting body, ball, seat, O-ring and gasket materials.
Why Chemical Processing Requires Special Valve Selection
Chemical processing systems expose valves to operating conditions that can be substantially more aggressive than ordinary water service. The medium may corrode metal surfaces, swell elastomer seals, attack valve seats or form crystals and deposits inside the valve cavity.
Even two systems carrying the same chemical can require different valves if their concentration or temperature is different. A material that performs well with a dilute chemical at ambient temperature may not provide acceptable service at higher concentration or elevated temperature.
Pneumatically actuated ball valves used in chemical plants therefore need to be evaluated as wetted-material systems rather than simply as actuator packages.
The body, ball, stem, seats, O-rings, gaskets and any internal lining must all be compatible with the process fluid.
How Pneumatically Actuated Ball Valves Work in Chemical Systems
Pneumatically actuated ball valves use compressed air to drive a quarter-turn actuator connected to the valve stem. The actuator rotates the ball approximately 90 degrees between the open and closed positions.
When the bore through the ball aligns with the pipeline, the valve allows fluid to pass. Rotating the ball places the solid portion across the flow path and isolates the chemical line.
A solenoid valve normally controls the compressed-air supply to the actuator. Limit switches can provide open and closed position feedback to the PLC or DCS, while a filter regulator helps maintain suitable actuator air pressure and air quality.
This configuration is useful in chemical plants because valves can be operated remotely during batch transfer, dosing, filling, draining and emergency process sequences.
Why Pneumatic Actuation Is Common in Chemical Plants
Pneumatic actuators provide relatively fast valve movement and can be configured with spring-return mechanisms for a predefined failure position. This makes them useful where a chemical line must automatically move toward a safe state if control air or power to the solenoid is lost.
Key Risks for Pneumatically Actuated Ball Valves in Chemical Processing
Corrosion
Corrosion can affect the valve body, ball, stem and fasteners. Stainless steel, thermoplastics or lined constructions may be required depending on the specific chemical.
Seat and Seal Attack
A chemically resistant body does not guarantee that the complete valve is compatible. Seats, stem seals and O-rings may fail before the valve body if they are exposed to incompatible chemicals.
Temperature
Chemical compatibility and mechanical strength can change significantly with temperature. This is particularly important for thermoplastic valves because their allowable pressure normally decreases as temperature increases.
Crystallization and Deposits
Some chemical solutions can crystallize or leave deposits when concentration, temperature or flow conditions change. Deposits around the ball and seat can increase operating torque and prevent complete shut-off.
Abrasive Solids
Suspended particles can damage soft seats or accumulate in the valve cavity. If solids content is significant, the valve construction and expected operating cycle should be reviewed carefully.
Pressure and Differential Pressure
Higher differential pressure increases the torque required to operate a ball valve. Pneumatic actuator sizing should therefore be based on actual valve torque under the maximum expected process conditions rather than nominal valve size alone.
Materials for Chemical-Service Pneumatically Actuated Ball Valves
Material selection should always be based on a chemical compatibility evaluation for the actual process conditions. The following materials represent common engineering options, but they are not universal recommendations for every chemical.
| Material | Typical Strength | Common Chemical-Service Use | Main Limitation to Check |
|---|---|---|---|
| SS304 | General corrosion resistance | Selected chemicals and general process fluids | Chlorides and aggressive acids |
| SS316 / CF8M | Improved corrosion resistance | Chemical transfer and process service | Specific acids, chlorides and concentration |
| UPVC | Corrosion-resistant thermoplastic | Acids, alkalis, salt solutions and chemical dosing | Temperature and pressure limits |
| CPVC | Higher-temperature thermoplastic option | Compatible corrosive chemical systems | Chemical-specific compatibility |
| PP | Lightweight chemical resistance | Selected acids, alkalis and treatment chemicals | Temperature and mechanical limits |
| PVDF | High chemical resistance | More aggressive compatible chemical service | Cost and exact media compatibility |
| PTFE | Broad chemical resistance | Seats, seals and lined valve components | Pressure, temperature and mechanical loading |
PTFE Seats
PTFE is widely used in chemical-service ball valves because it provides low friction and broad chemical resistance. However, temperature, pressure and mechanical loading must still remain within the valve manufacturer’s operating limits.
Elastomer O-Rings
EPDM, FKM and other elastomers can behave very differently in chemical service. The selected O-ring material should be checked separately from the valve body and PTFE seat.
Plastic vs Stainless-Steel Pneumatically Actuated Ball Valves
Both thermoplastic and stainless-steel pneumatically actuated ball valves can be used in chemical processing, but they address different operating envelopes.
| Factor | Plastic Ball Valve | Stainless-Steel Ball Valve |
|---|---|---|
| Corrosion Resistance | Excellent for many compatible chemicals | Depends strongly on alloy and chemical |
| Pressure Capability | Generally lower | Generally higher |
| Temperature Capability | Material dependent and more limited | Generally higher |
| Weight | Lightweight | Higher |
| Maintenance | Double-union designs can simplify removal | Depends on threaded or flanged construction |
| Typical Chemical Duty | Dosing, wastewater and corrosive transfer | Higher-pressure chemical process lines |
A plastic valve should not automatically be considered better for every corrosive chemical, and stainless steel should not automatically be considered suitable simply because it is metallic. The correct selection depends on the actual process medium and operating envelope.
Double Acting, Fail Close and Fail Open Pneumatic Ball Valves
Double-Acting Actuator
A double-acting pneumatic actuator uses compressed air for movement in both directions. This configuration is common where reliable instrument air is continuously available and a spring-return failure position is not required.
Fail-Close Configuration
A spring-return actuator can be arranged so the ball valve moves toward the closed position when the required air supply is lost. This may be appropriate when continued chemical flow would create an undesirable process condition.
Fail-Open Configuration
Some processes require the opposite response. For example, a process may need a cooling, flushing or relief path to remain open during a failure condition. In these cases, a fail-open configuration may be considered.
The correct failure position must be determined from the process safety philosophy. “Fail closed” is not automatically the safest choice for every chemical process.
Applications of Pneumatically Actuated Ball Valves in Chemical Processing
Pneumatically actuated ball valves can automate the isolation of acid, alkali, disinfectant and other chemical dosing lines. Compact plastic ball valves are frequently considered where the medium and operating conditions are compatible.
Acid-transfer systems require careful material selection because concentration and temperature can significantly change corrosion behavior. Thermoplastic, stainless-steel or lined valve constructions may be evaluated depending on the specific acid.
Caustic and alkaline process lines can use automated ball valves for storage-tank isolation, transfer and dosing. Valve body and elastomer compatibility should be confirmed for the exact concentration and temperature.
Neutralization systems often require multiple automated chemical feeds. Pneumatic ball valves can isolate individual reagent lines and operate as part of PLC-controlled dosing sequences.
Wet scrubber installations can expose valves to corrosive recirculation liquids and treatment chemicals. Plastic or corrosion-resistant valve materials may be appropriate depending on media composition and temperature.
Chemical wastewater systems may contain changing pH, dissolved salts and treatment reagents. Pneumatic automation allows isolation and routing to be integrated with treatment sequences while compatible valve materials help reduce corrosion problems.
Pneumatic ball valves can automate filling, draining and transfer between chemical storage tanks and process equipment. Spring-return operation can be considered when a defined failure position is required.
Fleyenda Pneumatic Ball Valve for Chemical Processing
For corrosive chemical transfer and dosing applications within suitable temperature and pressure limits, thermoplastic pneumatically actuated ball valves provide an alternative to conventional metal valves.
The FAT-Q-P combines a corrosion-resistant thermoplastic ball valve with a pneumatic rack-and-pinion actuator for automated chemical isolation.
The double-union body allows the valve section to be removed from the pipeline without cutting the piping, which can simplify maintenance in chemical dosing, treatment and process systems.
UPVC, CPVC, PP and PVDF body options allow the valve construction to be matched more closely to the process medium, while the actuator can be configured for double-acting or spring-return operation.
Typical applications: chemical dosing, acid and alkali transfer, salt solutions, wastewater treatment, corrosive chemical pipelines and automated process skids.
How to Select Pneumatically Actuated Ball Valves for Chemical Processing
1. Identify the Exact Chemical
Do not specify only “acid,” “alkali” or “chemical.” Provide the actual chemical name because different chemicals can attack the same valve material in very different ways.
2. Provide Concentration
Chemical concentration can significantly affect corrosion and seal compatibility. A valve suitable for a dilute solution may not be suitable for a concentrated process stream.
3. Confirm Temperature
Temperature affects both chemical compatibility and material strength. This is particularly important for plastic ball valves, where pressure capability and dimensional stability can change with increasing temperature.
4. Specify Pressure and Differential Pressure
Provide normal operating pressure, maximum pressure and maximum differential pressure. Differential pressure influences the torque required from the pneumatic actuator.
5. Select All Wetted Materials
Confirm body, ball, stem, seat, O-ring, gasket and lining materials rather than focusing only on the valve-body material.
6. Define the Failure Position
Determine what should happen when instrument air or control power is lost. The required failure mode should be based on the plant’s process safety strategy.
7. Check Air Supply
Pneumatic actuator sizing should use the minimum reliable air pressure available at the valve location rather than the maximum compressor pressure.
8. Consider Maintenance Access
Double-union plastic valves can be attractive on smaller chemical lines because they allow valve removal without cutting the piping. Flanged or multi-piece metal ball valves may be more appropriate in other process systems.
Chemical-Service Pneumatic Ball Valve RFQ Checklist
- Chemical name
- Chemical concentration
- Valve size / DN / NPS
- Normal operating pressure
- Maximum pressure
- Maximum differential pressure
- Minimum and maximum temperature
- Flow direction and required valve function
- Body material
- Ball and stem material
- Seat material
- O-ring and gasket material
- Pipeline connection
- Available compressed-air pressure
- Double acting or spring return
- Required fail-open or fail-closed position
- Solenoid valve voltage
- Limit-switch feedback
- Explosion-proof accessory requirement if applicable
- Required quantity
Common Chemical Valve Selection Mistakes
| Mistake | Possible Result | Better Approach |
|---|---|---|
| Specifying only “acid” or “chemical” | Wrong material selection | Provide exact chemical and concentration |
| Checking body material only | Seat or O-ring failure | Review all wetted materials |
| Ignoring temperature | Reduced pressure capability or accelerated attack | Evaluate compatibility at actual temperature |
| Oversizing pneumatic actuator by guesswork | Unnecessary cost or incorrect operation | Use actual valve torque and air pressure |
| Using a plastic valve above its operating envelope | Deformation or leakage risk | Check material-specific pressure and temperature limits |
| Assuming fail-close is always safest | Incorrect process response during failure | Determine safe state from process design |
| Ignoring deposits or crystallization | High torque or incomplete closure | Review process chemistry and cleaning strategy |
Pneumatically Actuated Ball Valves for Chemical Processing FAQs
Are pneumatically actuated ball valves suitable for chemicals?
Yes. Pneumatically actuated ball valves are widely used in chemical processing, but the valve body, ball, seat, O-rings and seals must all be compatible with the exact chemical, concentration and temperature.
What ball valve material is best for corrosive chemicals?
There is no single best material. Depending on the chemical and operating conditions, options may include SS316, UPVC, CPVC, PP, PVDF or fluoropolymer-lined constructions.
Are plastic pneumatic ball valves suitable for acid?
Plastic ball valves can be suitable for many compatible acids, but acid type, concentration, temperature and pressure must be checked against the selected thermoplastic material.
Can pneumatic ball valves be used for alkali solutions?
Yes, provided all wetted materials are compatible with the specific alkali concentration and operating temperature.
What is the advantage of a double-union plastic ball valve?
The union connections allow the valve body to be removed from the pipeline for inspection or replacement without cutting the piping, which can simplify maintenance in chemical dosing and treatment systems.
Should chemical ball valves be fail closed?
Not always. Fail-close is appropriate for some applications, but other processes may require fail-open operation. The failure position should be determined by the plant’s process safety requirements.
What air pressure is required for pneumatic ball valves?
The required pressure depends on actuator and valve torque. The Fleyenda FAT-Q-P configuration shown above specifies a pneumatic air-source range of 3–8 bar.
Can a pneumatic ball valve be controlled by a PLC?
Yes. A solenoid valve can receive PLC commands, while limit switches can provide valve-position feedback. Positioners can be added when intermediate positioning is required.
What information should I provide when ordering a chemical ball valve?
Provide the exact chemical, concentration, pressure, temperature, valve size, connection, required wetted materials, air pressure, actuator function, failure position and control accessories.
Need Pneumatically Actuated Ball Valves for a Chemical Process?
Chemical valve selection should begin with the actual process medium rather than a generic valve specification. Material compatibility, concentration, temperature, pressure and actuator failure mode can all change the correct solution.
Fleyenda supplies pneumatic valve configurations for chemical dosing, corrosive liquid transfer, wastewater treatment, process skids and industrial chemical systems.
For technical selection, send the chemical name, concentration, valve size, pressure, temperature, connection, available air pressure, fail position and quantity.
Choosing Pneumatically Actuated Ball Valves for Chemical Processing
Pneumatically actuated ball valves provide fast, automated isolation for chemical transfer, dosing, tank switching and process-control systems, but chemical service requires much more careful valve selection than general utility applications.
The most important consideration is chemical compatibility. Body material alone is not enough; seats, seals, O-rings, stems and other wetted components must also withstand the actual chemical concentration and operating temperature.
Thermoplastic valves such as UPVC, CPVC, PP and PVDF can provide useful corrosion resistance in suitable chemical applications, while stainless-steel and other metallic constructions may be more appropriate where higher pressure or temperature capability is required.
The pneumatic actuator must then be sized according to actual valve torque and available air pressure, with the correct double-acting or spring-return failure configuration selected according to the process safety philosophy.
For chemical processing projects, specifying the valve and actuator as one engineered package provides a more reliable basis for corrosion resistance, automation performance and long-term maintenance.